
Steel guide
Carbon or stainless
Both are DSC® SuperClean Damascus from BALBACHDAMAST® (opens in a new tab). Carbon hardens in oil and needs oiling; stainless hardens under vacuum or protective gas and is food-safe.
| Side by side | 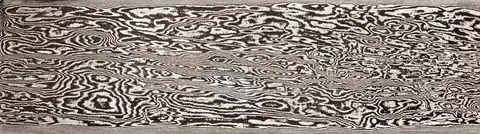 DSC® Carbon | 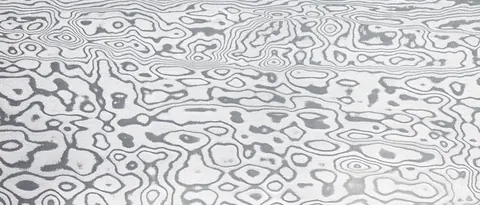 DSC® Inox |
|---|---|---|
| Steels | 1.2842 datasheet (opens in a new tab) + 1.2767 datasheet (opens in a new tab) | 1.4034 datasheet (opens in a new tab) + 19C27 datasheet (opens in a new tab) |
| Grades | AISI O2 + AISI 6F7 | AISI 420C + Alleima 19C27 |
| Layers | 160 | 120 |
| As delivered | Soft annealed, 22-27 HRC | Soft annealed, 22-27 HRC |
| Max hardness | Up to 62-63 HRC | Up to 62 HRC |
| Forging | 1742-1976°F | 1742-1922°F |
| Hardening | 1544°F, oil quench | 1922-1976°F under vacuum or protective gas, air quench |
| Deep freeze | Recommended | Recommended, right after the quench |
| Temper | 2 × 1 hr at 356°F, 62 HRC | 2 × 0.75 hr at 356-374°F, 60-61 HRC |
| Etchants | FeCl₃ or H₂SO₄ | H₂SO₄ only |
| Care | Keep it oiled | Stainless, food-safe |
| Patterns in stock | 8 | 7, no Herringbone |
| Cut to size from | $2.25 / in | $3.25 / in |
The steel numbers link to each grade's datasheet: Dörrenberg Edelstahl for 1.2842, 1.2767 and 1.4034, Alleima for 19C27.
Choose carbon if
- You harden with an oil quench from a forge or a basic kiln.
- You want the most hardness out of the steel.
- You don't mind keeping the blade oiled.
Choose stainless if
- You can harden under vacuum or protective gas, then deep freeze.
- The knife will see food, water or weather.
- You want a blade that asks for less care.
Heat treatment
From the forge to the temper
DSC® Carbon
- 01
Forge · 1742-1976°F
950-1080°C. Cool slowly after forging.
- 02
Anneal · only after hot work
2 hr at 1328°F (720°C), then 2 hr at 1202°F (650°C). Cool in the furnace, remove below 570°F (300°C).
- 03
Harden · 1544°F, oil
840°C, 4 min soak, quench in oil. Deep freeze recommended, not required.
- 04
Temper · 2 × 1 hr
356°F (180°C) for knife blades: 62 HRC. 392°F (200°C) for decorative pieces: 61 HRC.
DSC® Inox
- 01
Forge · 1742-1922°F
950-1050°C. Cool slowly after forging.
- 02
Anneal · only after hot work
At least 4 hr at 1526°F (830°C). Cool in the furnace, remove below 752°F (400°C).
- 03
Harden · 1922-1976°F
1050-1080°C under vacuum or protective gas, 15-20 min soak. Quench in air. Steel makers' note: stay near the low end, about 1940°F (1060°C), the temperature on Alleima's 19C27 sheet; the 1.4034 sheets stop at 1922°F (1050°C). Air quench works for thin stock; thicker billets want quench plates or a fast gas quench, because 19C27 has to drop below 1112°F (600°C) within about 2 minutes.
- 04
Deep freeze · right after the quench
The mill's hardening steps deep freeze straight after the air quench. Recommended, not required. Steel makers' note: about -94°F (-70°C), with no hold once it gets there.
- 05
Temper · 2 × 0.75 hr
356-374°F (180-190°C) for knife blades: 60-61 HRC. 2 hr at 572°F (300°C) for decorative pieces: 56-57 HRC. You can deep freeze again before the second temper.
From the BALBACHDAMAST® datasheets. The stainless notes marked "steel makers' note" come from the datasheets for 1.4034 and Alleima 19C27. Every product page carries the full schedule. Step by step for carbon, with what to expect at each stage: the carbon Damascus heat treatment guide.
Etching
Bring the pattern up
DSC® Carbon
- 01
Prep
Fine polish, up to a mirror, after hardening. Degrease with dish soap or acetone.
- 02
Etch at 122°F (50°C)
FeCl₃ 15-35% or H₂SO₄ 15-30%, warmed in a water bath.
- 03
Passes
Etch until the layers clearly show. Light: 20-40 sec passes. Deep: 4 × 5 min. Toothbrush and baking soda between passes.
- 04
Finish
Neutralize, then fine polish or sand above 2000 grit until the contrast is where you want it. Oil or wax to finish.
DSC® Inox
- 01
Prep
Fine polish, up to a mirror, after hardening. Degrease with dish soap or acetone.
- 02
Etch at 122-140°F (50-60°C)
Fresh H₂SO₄ 15-20%, warmed in a water bath. Sulfuric cuts about 5 µm every 5 min; 20 min gives a deep etch.
- 03
Finish
Neutralize, then fine polish above 2500 grit until the contrast is where you want it.
- 04
Never on stainless
No ferric chloride. No muriatic acid.
More in the etching guide.
Meteorite, titanium and mokume are on the rare and custom Damascus page.
Stainless rounds and ring slices for jewelers are on the Damascus for rings and jewelry page.
Sizes
Millimeters to inches
1 IN = 25.4 MM · LENGTHS ARE CUT TO THE INCH
| Width (mm) | Inches |
|---|---|
| 20 | 0.79 |
| 25 | 0.98 |
| 30 | 1.18 |
| 35 | 1.38 |
| 40 | 1.57 |
| 45 | 1.77 |
| 50 | 1.97 |
| 55 | 2.17 |
| 60 | 2.36 |
| Thickness (mm) | Inches |
|---|---|
| 2 | 0.08 |
| 2.5 | 0.10 |
| 3 | 0.12 |
| 4 | 0.16 |
| 5 | 0.20 |
| 6 | 0.24 |
| 8 | 0.31 |
| 10 | 0.39 |